Overview
A Nebraska facility needed to replace an existing overhead crane and extend its lifting coverage into an expanded work area. However, combustible dust within the facility created a classified hazardous environment.
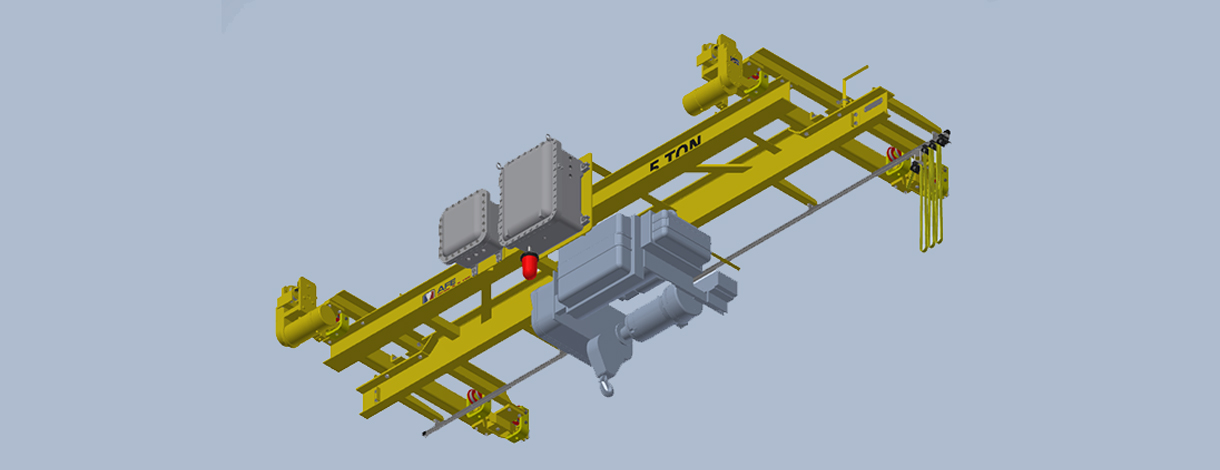
AFE Crane designed and installed a 5-ton explosion-proof overhead crane for the application. The project also extended the existing runway from 60 feet to 120 feet. This provided crane access to new machinery within the expanded area.
The new system used ACCO equipment configured for a Class II, Group G, Division I environment.
Project Challenges
The hazardous environment was the primary consideration for the new crane system. Combustible dust required equipment appropriate for the facility’s Class II, Group G, Division I classification.
The existing motorized underhung single-girder crane dated to 1999. Therefore, the project required AFE Crane to replace the crane while working within the existing building conditions.
The facility expansion created another challenge. New machinery extended beyond the reach of the original 60-foot runway. As a result, AFE Crane needed to double the runway length to 120 feet.
Headroom also affected equipment selection. The application required a long lift while preserving the available vertical space.
The AFE Crane Solution
AFE Crane designed and installed a 5-ton Class II, Group G, Division I explosion-proof crane. The crane included a 14-foot span and a 17-foot, 6-inch patented track bridge.
An ACCO-Wright electric wire rope hoist provided 66 feet of lift. The hoist operated at a single lifting speed of 30 feet per minute. This configuration provided the required lifting speed while working within the available headroom.
The trolley operated at a single speed of 50 feet per minute.
AFE Crane specified hoist components labeled for the classified environment. These included the motor, motor brake, and conduit fittings. The Work-Rated hoist also included an overload device and a Weston-style mechanical load brake.
Radio remote controls allowed operators to control the crane and hoist away from the load.
Project Execution
AFE Crane assembled and tested the crane components before installation. The installation team then coordinated with the facility to integrate the new equipment into the existing space.
The system used ACCO-Louden 585-style end trucks. Each assembly included eight 4.5-inch-diameter wheels, steel wheel drives, and a 6-foot wheelbase.
AFE Crane also incorporated dual gimbal rod assemblies into the runway suspension system. This configuration allowed movement within the supporting structure while maintaining the under-running crane runway.
The completed project replaced the existing crane and extended the runway from 60 feet to 120 feet. As a result, the new crane could serve equipment within the expanded work area.
Conclusion
Hazardous manufacturing environments require careful consideration of both the lifting application and the surrounding conditions.
For this facility, AFE Crane needed to address several requirements at the same time. The crane had to provide a 5-ton capacity and 66 feet of lift. It also needed to operate within a Class II, Group G, Division I environment and reach new machinery within an expanded work area.
AFE Crane addressed these requirements with an explosion-proof overhead crane and a 120-foot runway system. The project also incorporated labeled electrical components, an overload device, mechanical load brake, radio controls, and a suspension system designed around the existing building conditions.
Learn More About Explosion Proof Overhead Cranes Here
Contact AFE Crane
If your facility requires overhead lifting equipment for a classified or hazardous environment, AFE Crane can help. Our engineering team can evaluate the load, facility conditions, hazardous-area classification, available headroom, required coverage, and lifting requirements.
Whether your application requires an explosion-proof overhead crane, runway extension, specialized hoist, or another engineered lifting system, AFE Crane provides engineering, equipment integration, installation, startup, and long-term support.
Contact AFE Crane to discuss your next explosion-proof crane project.